The repeated loading, vibration, corrosion, fatigue, and strenuous operating conditions are forces that expose industrial equipment and structures to pressure. Very small cracks on the surface that are not noticeable may one day grow into severe failures, especially in important parts like welds, shafts, lifting equipment, pressure-containing parts, and structural connections. This is the reason why Non-Destructive Testing (NDT) is a great consideration in industrial maintenance and inspection programmes.
Magnetic particle inspection is an NDT technique that is commonly used to detect surface and near surface discontinuities in ferromagnetic materials. It can show flaws that might not be seen in a normal visual check, and assist inspection teams to make a better judgment of what needs to be repaired, whether to operate, and the condition of the assets. Embedded in a formal inspection system, such a technique can be used to facilitate Crack Detection, Weld Inspection, and long-term Asset Integrity Management in both industrial and offshore systems.
Magnetic particle inspection is a form of NDT that employs a magnetic field and a set of specially prepared magnetic particles to identify discontinuities in materials that are ferromagnetic.
The component is inspected by being magnetized. When a crack or other discontinuity breaks the magnetic field, magnetic flux leakage takes place around the defect. Magnesium particles that are fine in nature deposited on the surface concentrate around this leakage field and form a visible indication that, in turn, can be assessed by a qualified inspector.
The technique is regularly applied to carbon steel and other ferromagnetic materials in which the surface or a little bit below the surface defects have to be detected.
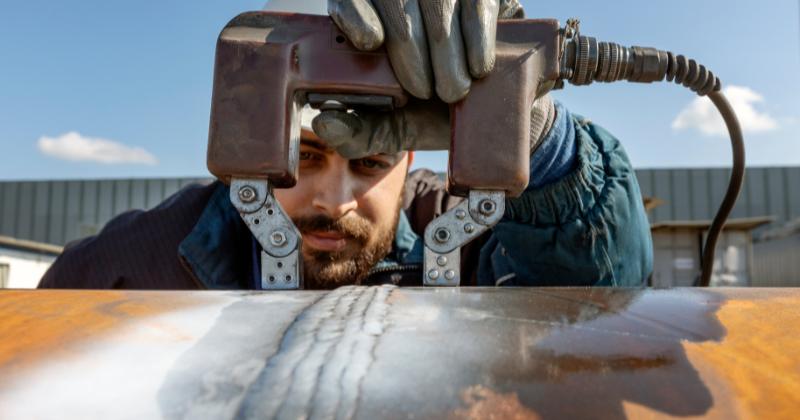
A normal check-up is characterized by a number of inspection steps.
The part is washed to eliminate dirt, grease, scale, paint, or other contaminants which may disrupt the check. Preparation of surfaces enhances the visibility and quality of indications.
An appropriate magnetic field is added to the component. The orientation of the magnetization is significant since in this way the defects are best identified when oriented approximately perpendicular to the magnetic field.
Magnetic particles, either dry powder or wet, are applied when the component is magnetized. The particles are concentrated at the sites where the magnetic flux leakages take place.
Indication Evaluation
The inspector analyzes the patterns of the particles and decides on whether they are indicative of relevant discontinuities, surface conditions, or non-relevant indicators.
Demagnetization and Cleaning
The component can be demagnetized and cleaned as per the respective procedure after the examination.
The main advantage of this method is Crack Detection on the material surface and near the surface.
Common discontinuities are fatigue cracks, grinding cracks, seams, laps, and lack of fusion, as well as some imperfections associated with welding. It is also able to detect defects near areas of stress concentration like keyways, threads, fillets, and weld toes.
The method is limited, though. It is not applicable, with much success, to non-ferromagnetic materials like most aluminium, copper, and austenitic stainless steels. It also fails to give the same information on depth as methods that are specifically used in volumetric examination.
When choosing the right NDT method, it is important to understand these limitations.
Welded joints may undergo considerable stresses both in fabrication and service. Appropriate Weld Inspection assists in locating discontinuities that may influence the structural performance.
The method may be especially effective in investigating weld toes, weld caps, heat-affected regions, and other regions where surface-breaking or near-surface defects may occur.
In the majority of cases, it is applied in conjunction with other inspection methods, instead of being a complete examination of vital elements. This multi-methodology offers a more comprehensive insight on weld condition.
Surface Defect Detection is especially significant when it comes to components that undergo cyclic loads or high operating stresses. Over a period of time, shafts, gears, hooks and lifting accessories, pressure parts, and structural members may develop fatigue-related cracking.
Defects can be detected during regular inspections, before they become significant integrity issues. The time of inspection must be set based on the importance of the equipment, the nature of the working environment, loading history, the relevant regulations, and past inspection results.
Asset Integrity Management is the management of equipment and structures to ensure that they are in a condition to support their intended operation safely during their lifetime of service.
The outcomes of inspection can help in this process by giving details on the status of vital components. By documenting the results and comparing them over time, the organizations can determine the locations of frequent defects, track the wear and tear, and enhance the maintenance planning.
In offshore, marine, oil and gas, construction and heavy engineering, NDT findings can be used to incorporate into an asset integrity strategy to minimize unexpected failures and enhance lifecycle management.
There is no universal technique of inspection applicable to all materials or defects. The selection of the right technique is based on the component, material, anticipated defect, inspection purpose, and sensitivity necessary.
Ultrasonic testing is usually chosen when defects in the interior or the thickness of the material are to be tested. Dye penetrant testing is applicable in identifying surface-breaking defects on the appropriate non-porous material. The visual inspection is still a significant first-order technique for detecting the evident surface conditions.
In ferromagnetic parts where surface and near-surface fractures are of primary interest, magnetic particle inspection may offer a very useful inspection.
The level of quality of inspection is also based on the equipment and the process as well as the competence of the staff conducting the test.
The organizations must have inspections that are conducted following proper procedures, equipment that is well maintained, magnetic particles that are suitable, the surface is well prepared, and the personnel are qualified. The chosen magnetization method ought to be aligned to the anticipated defect orientation, and the lighting and viewing circumstances ought to be apt to assess indications.
The records of inspection should also be kept in a manner that the major discoveries can be examined in later maintenance and integrity checks.
Ans: It is mainly applied to identify surface and near-surface discontinuities in ferromagnetic materials, especially cracks, and some defects related to welds.
Ans: It is best used on surface and near-surface defects. Ultrasonic, or other volumetric NDT methods, can be more suitable to address deeper internal discontinuities.
Ans: This technique is intended to be used in ferromagnetic substances like carbon steel, low-alloy steel, and some iron-based alloys. It is not typically applicable to non-ferromagnetic materials.
Ans: No. It is a Non-Destructive Testing (NDT) technique, i.e., the part is not deliberately damaged in the process of testing.
Ans: It is able to detect cracks and near-surface cracks and other discontinuities near the welds and assist the inspectors in assessing the areas that can be prone to fatigue or other stress-induced damages.
Ans: The correct time interval varies based on the criticality of equipment, the conditions of service, loading, the standards that are relevant, the past discoveries, and the inspection program of the organization. Most vital aspects might have to be examined more often.
Finding cracks and material discontinuities early is key to safe and reliable industrial assets. This NDT method plays a significant role in industrial inspection programs by offering successful Crack Detection, supporting Weld Inspection, and detecting surface and near-surface discontinuities in appropriate materials.
Combined with other Non-Destructive Testing (NDT) tools and a comprehensive approach to Asset Integrity Management, magnetic particle inspection can assist organizations in detecting possible issues prior to their escalation into expensive failures. In offshore, marine, oil and gas, construction and heavy engineering applications, the identification of the suitable inspection method and adherence to qualified procedures are important in ensuring the safety of assets and the long-term operational performance of the assets.